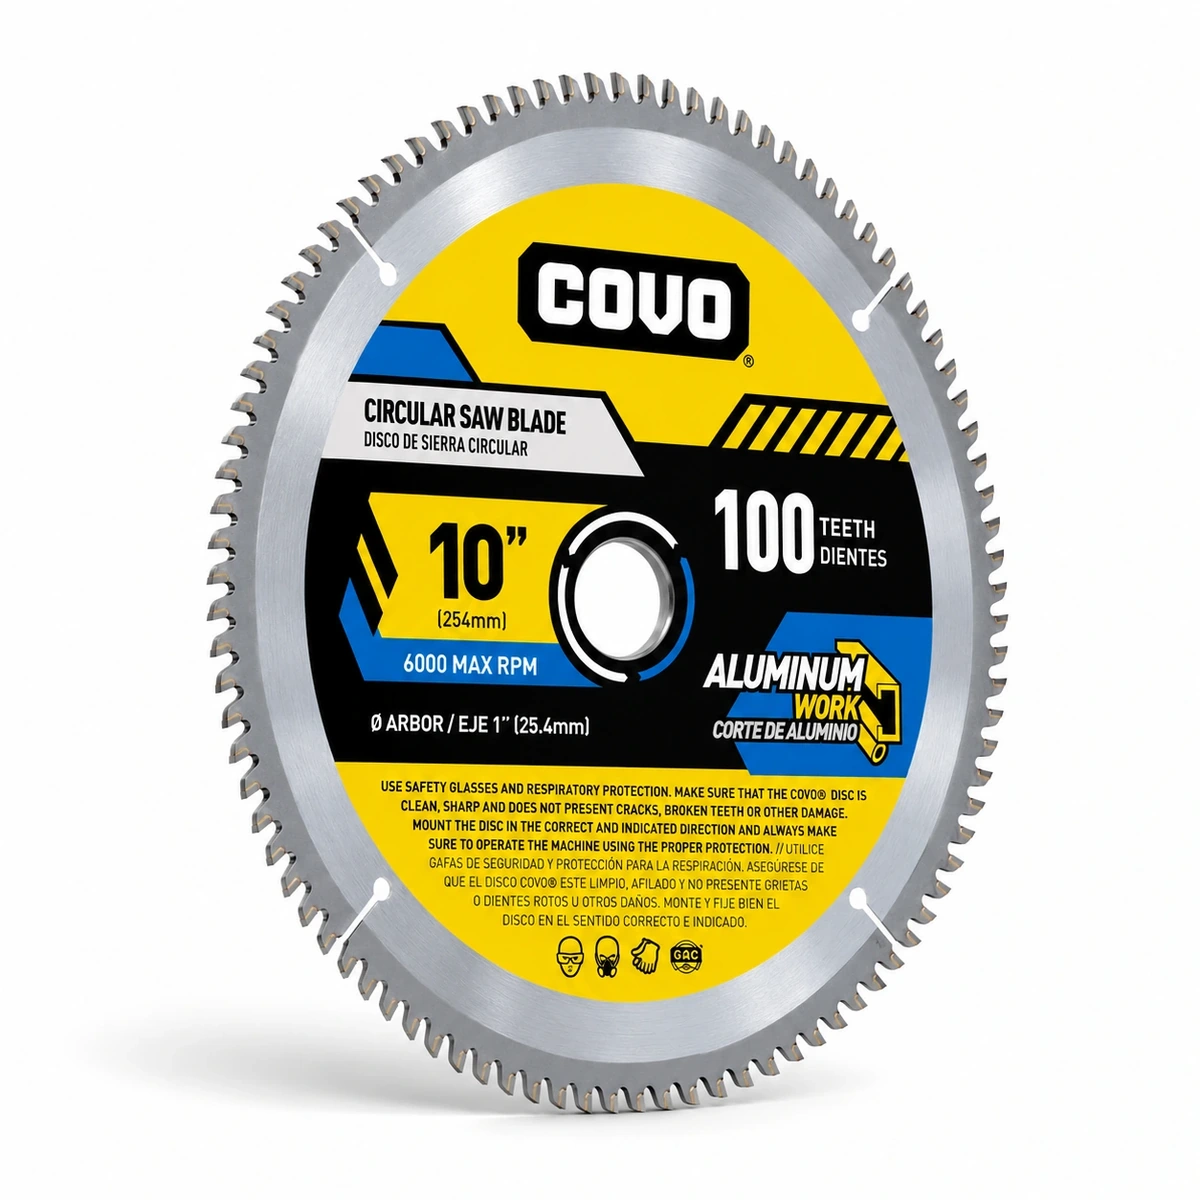
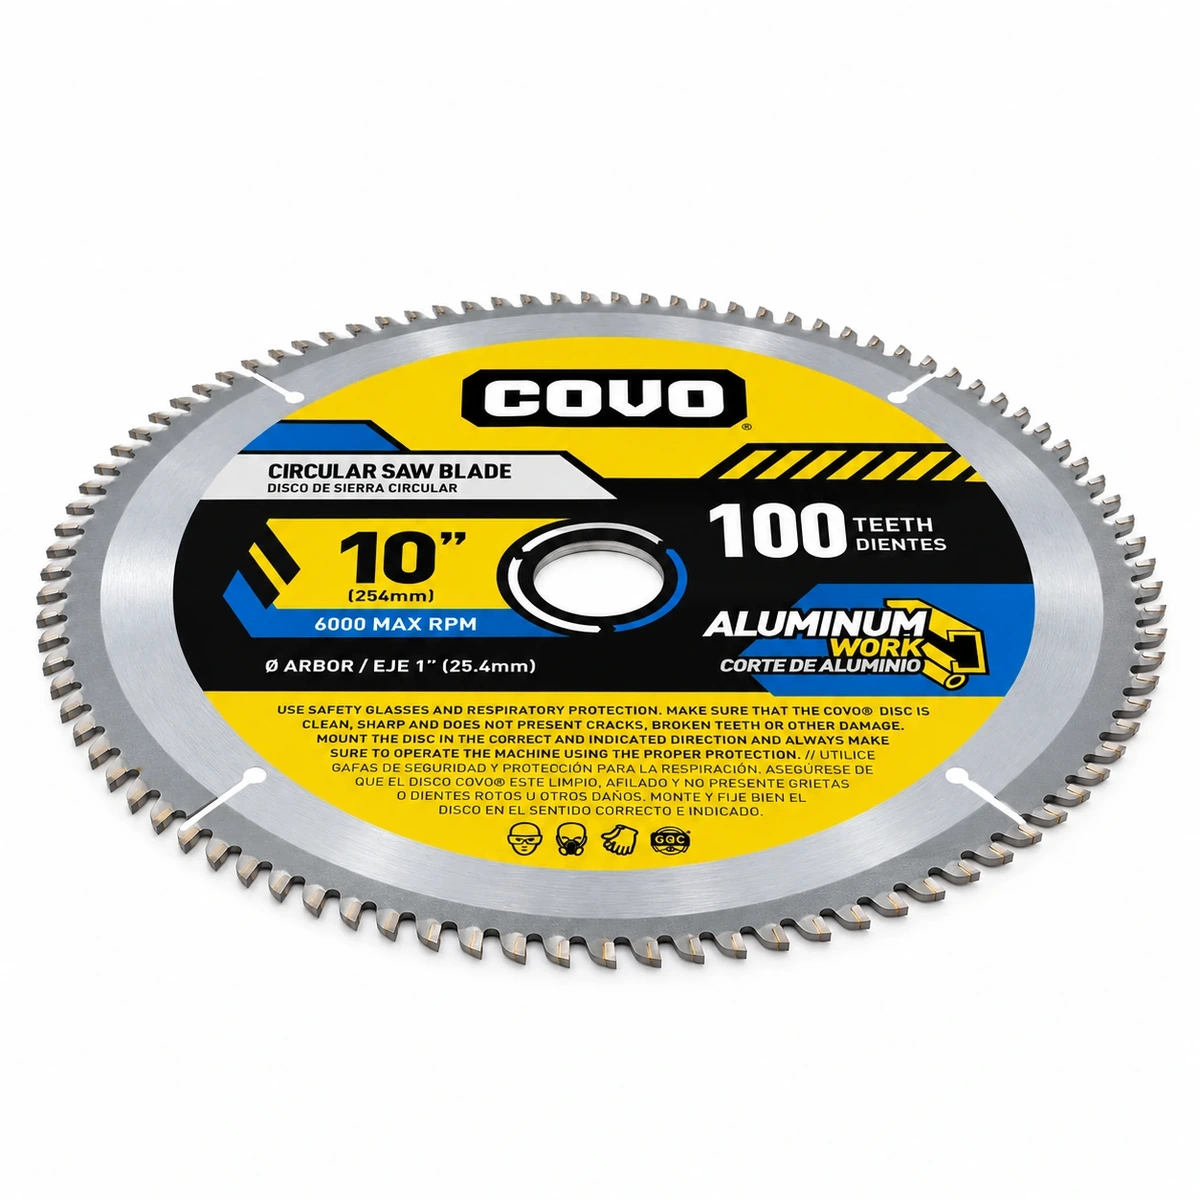
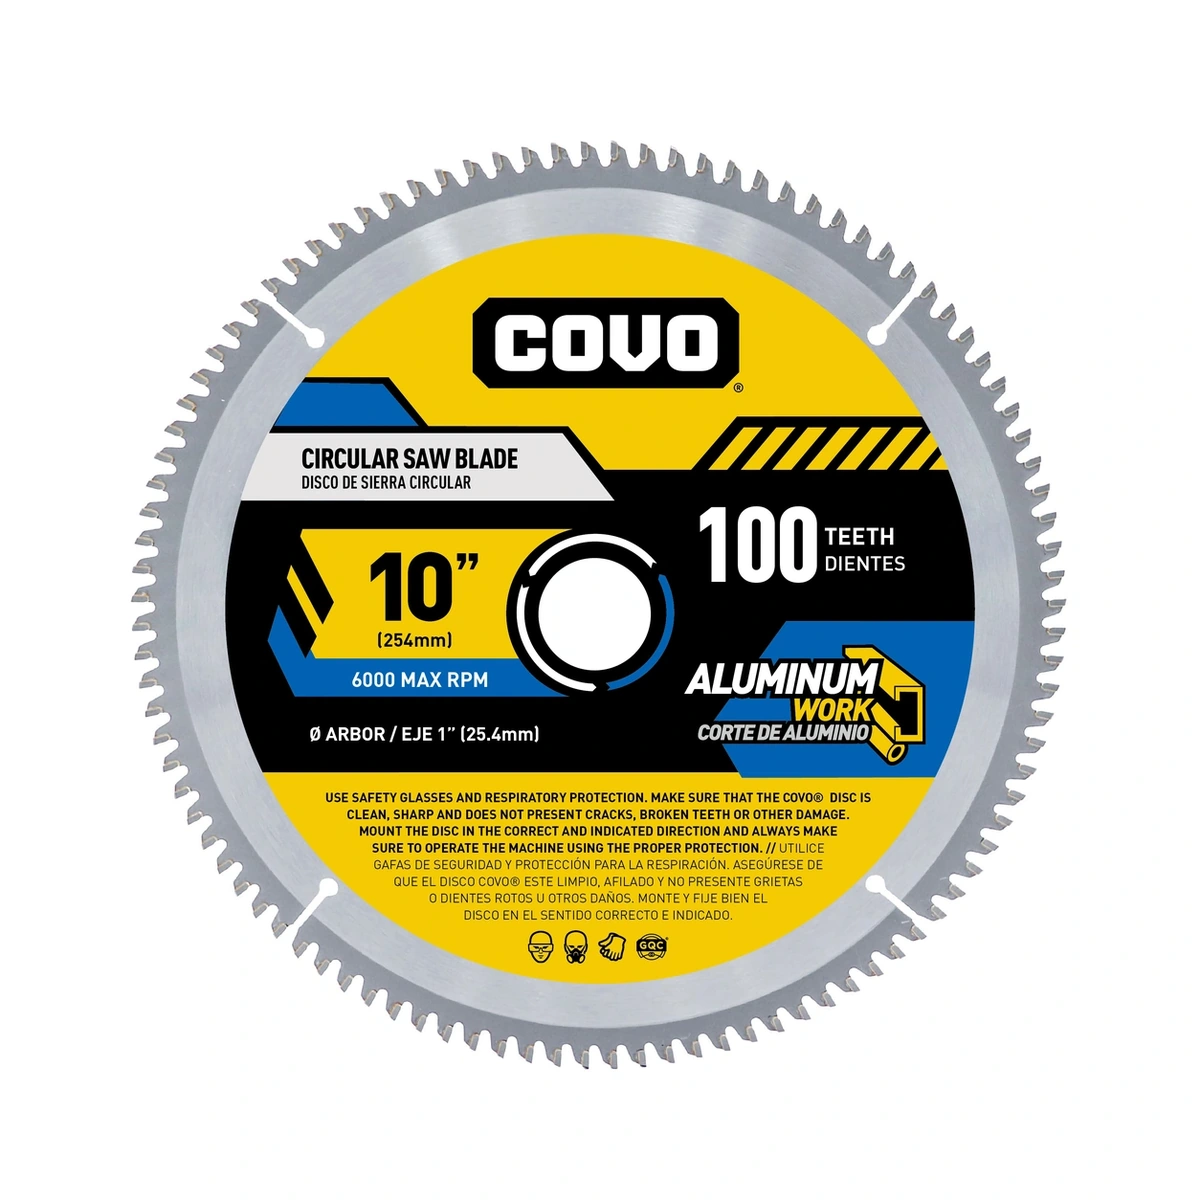
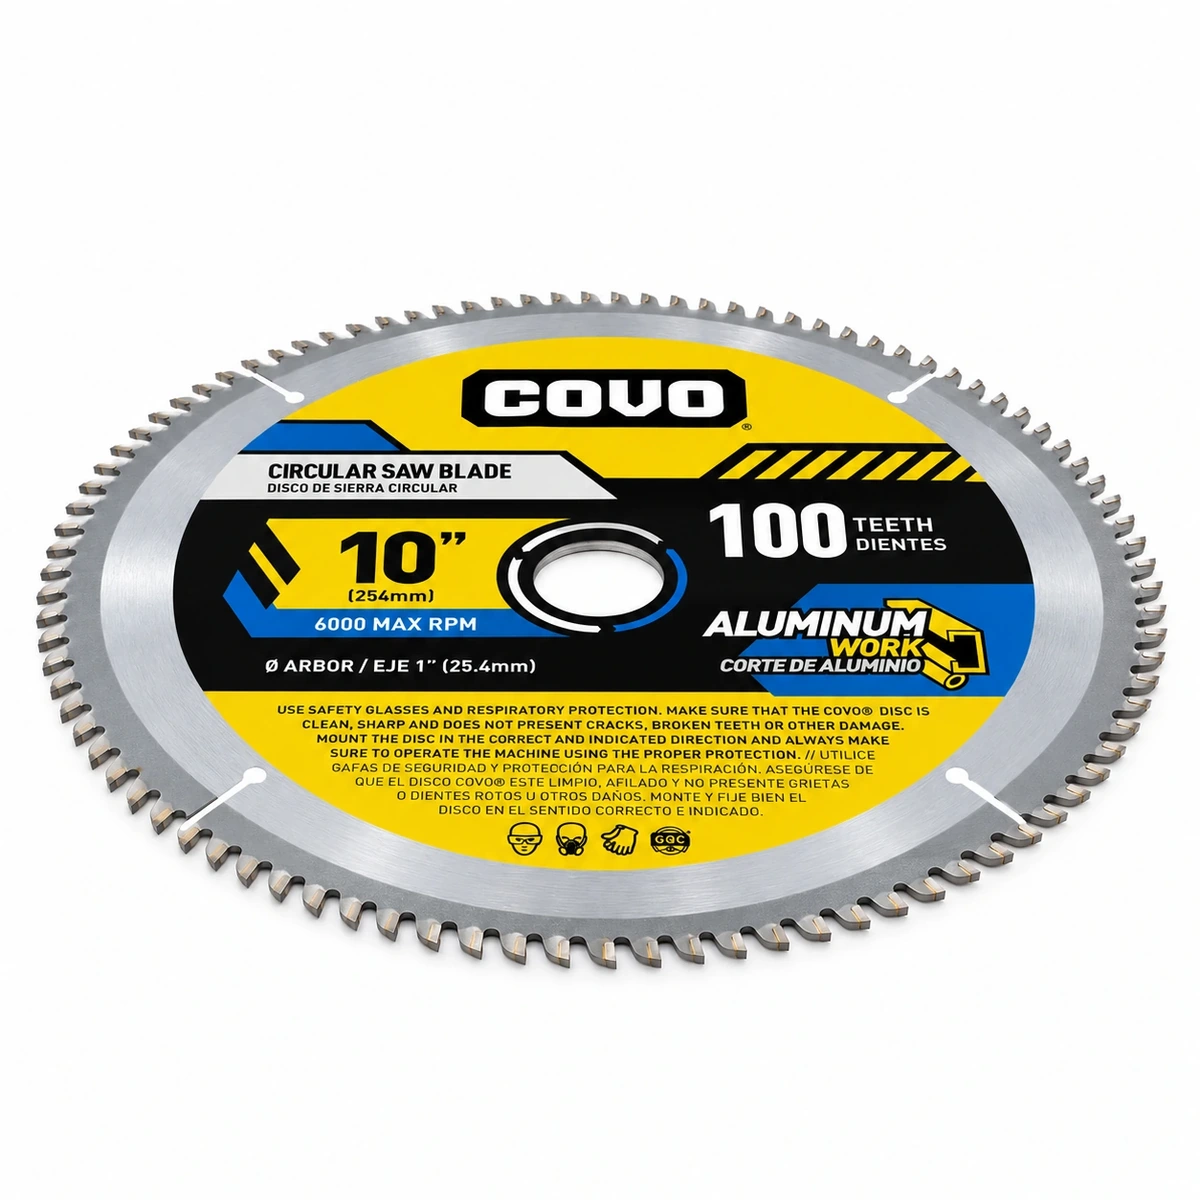
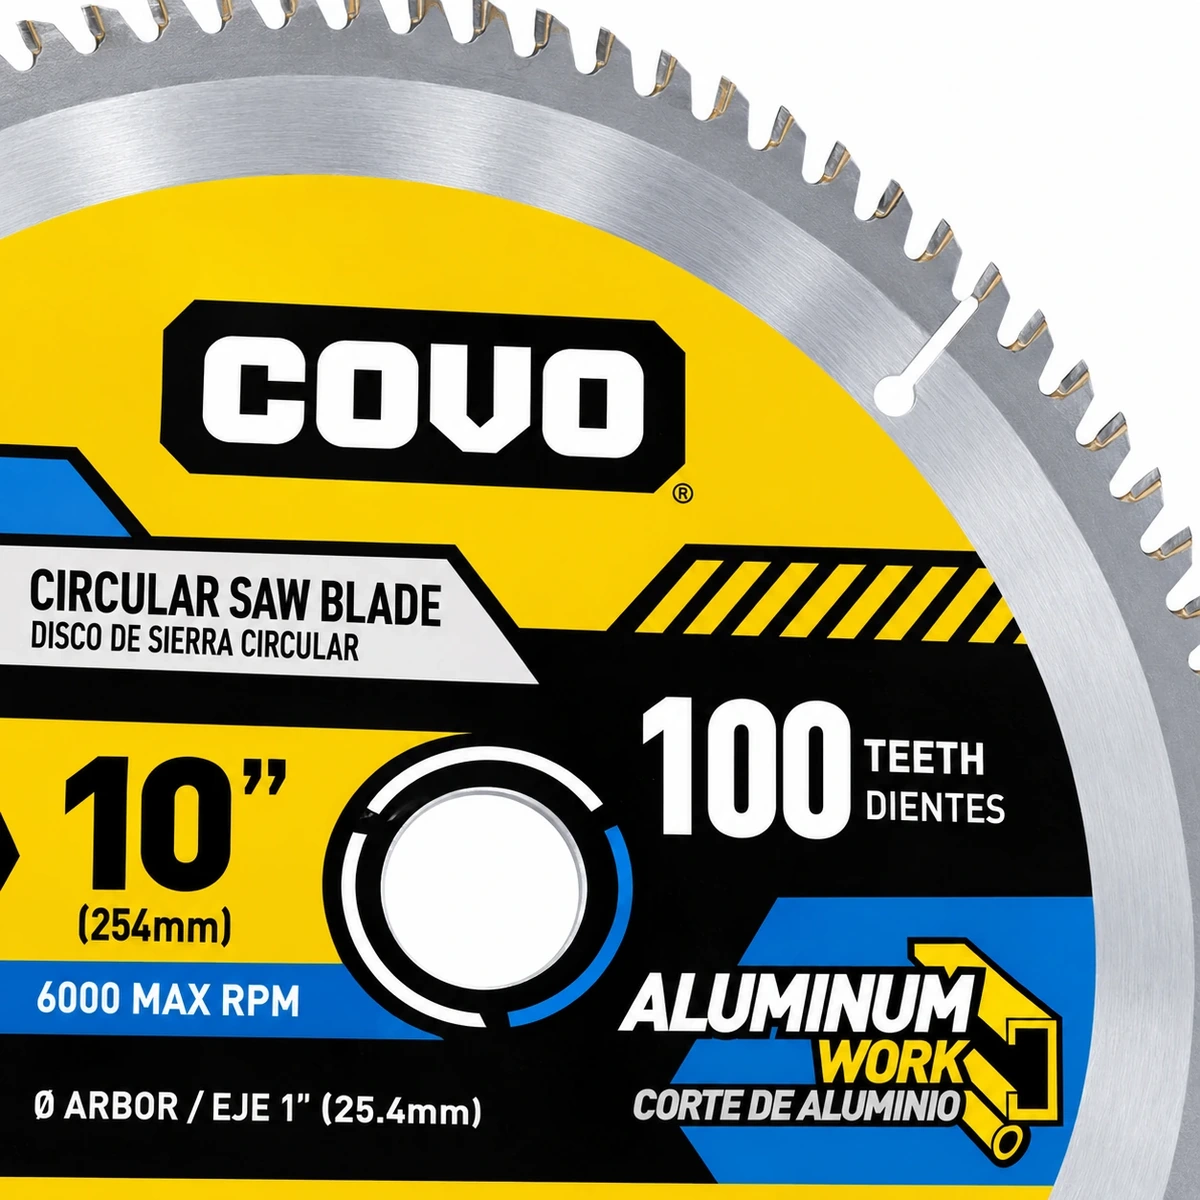
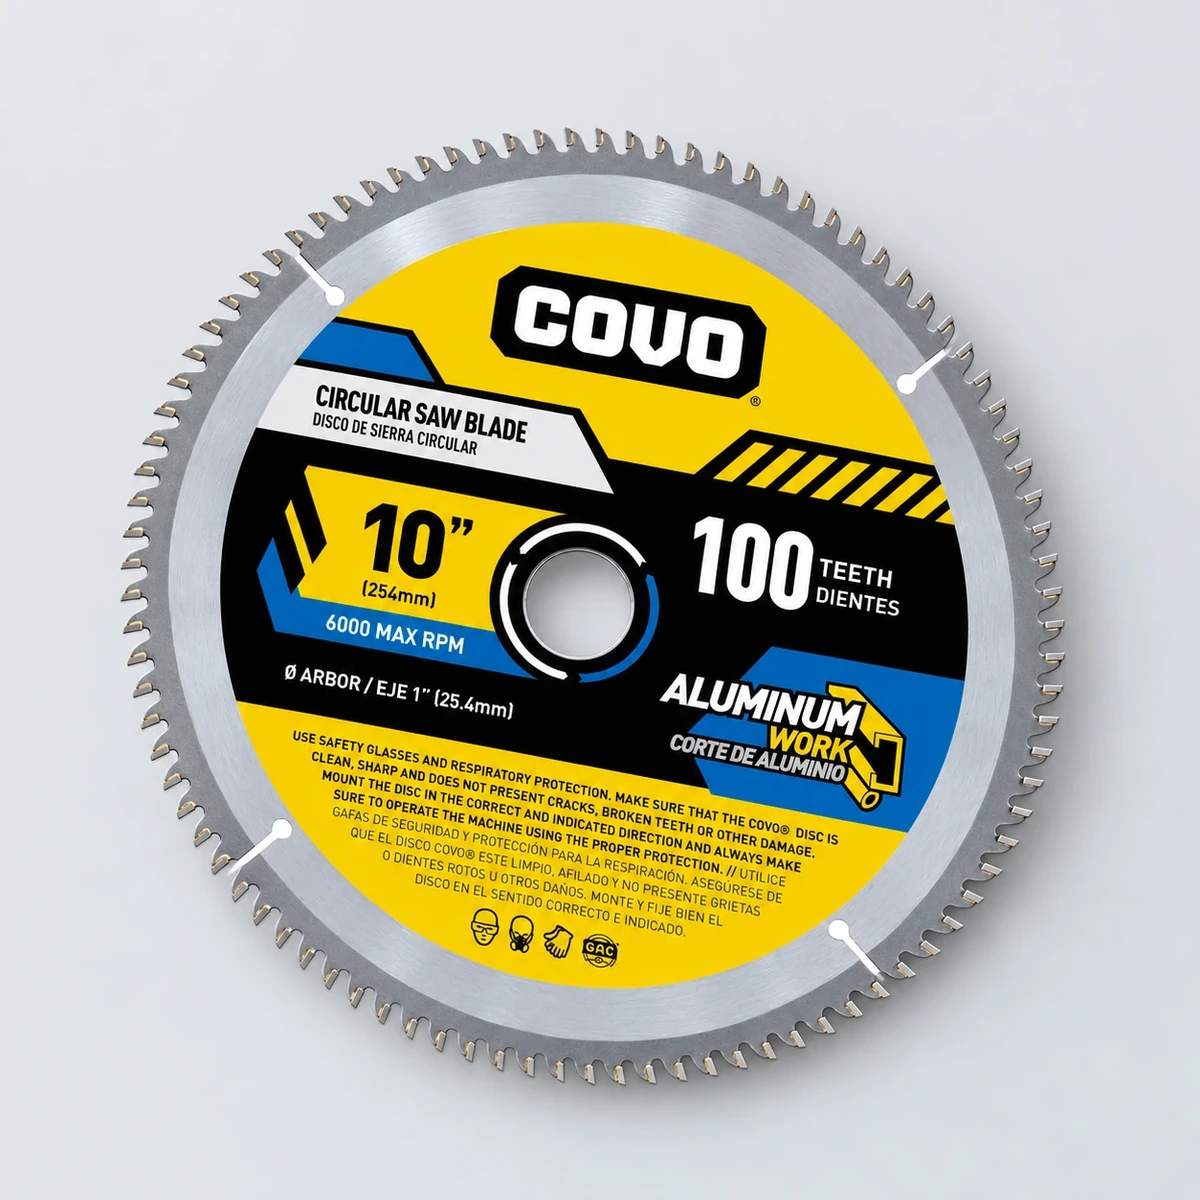
Product Specifications
Specification | Details |
Blade Diameter |
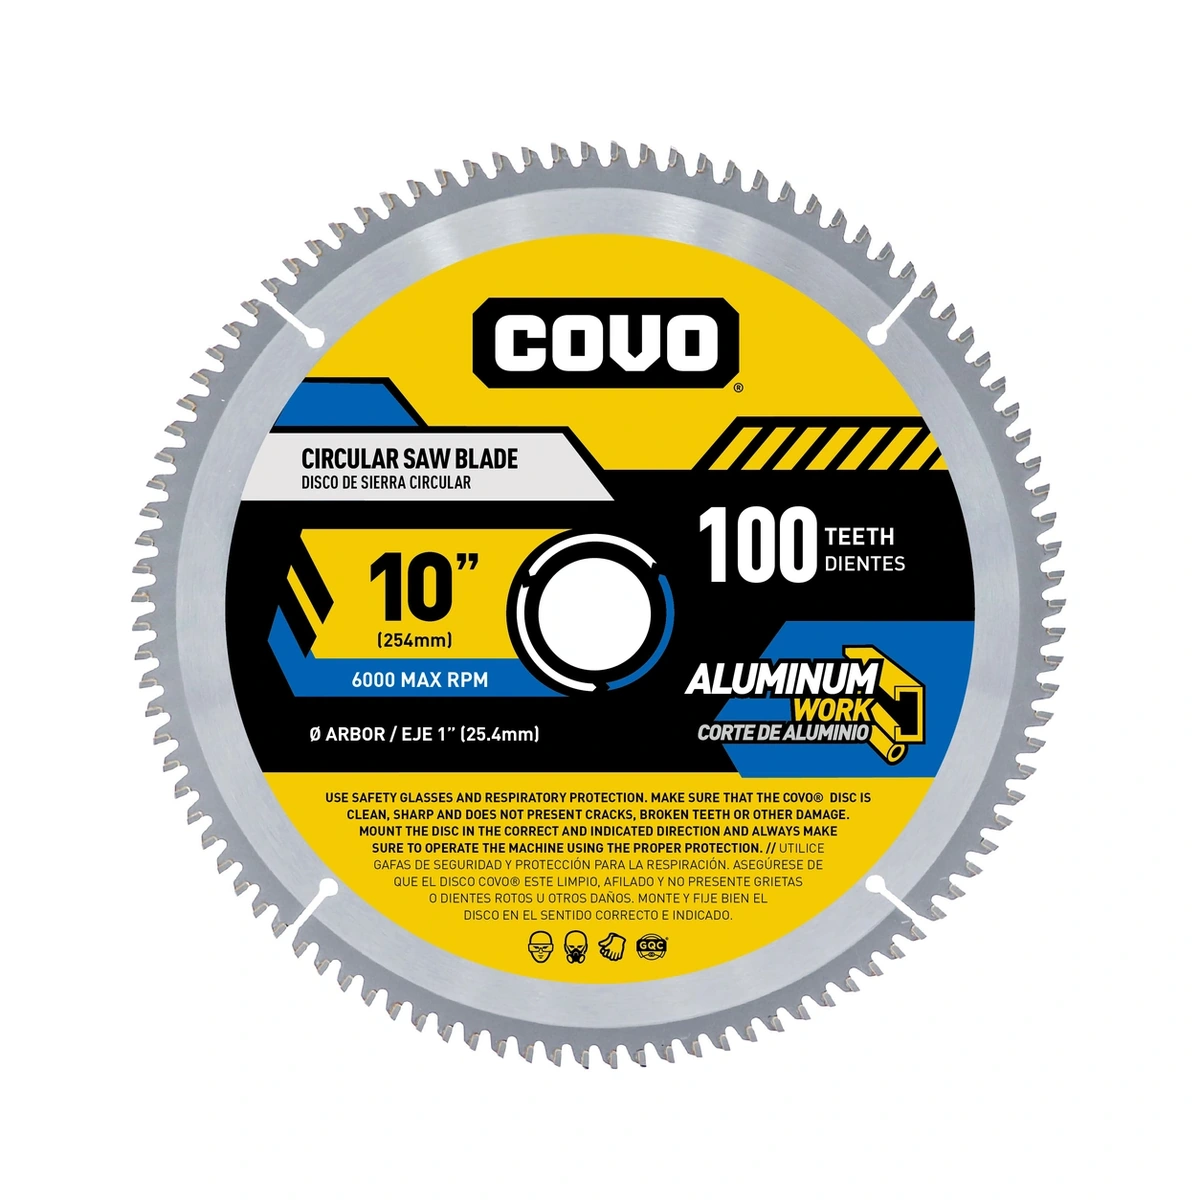
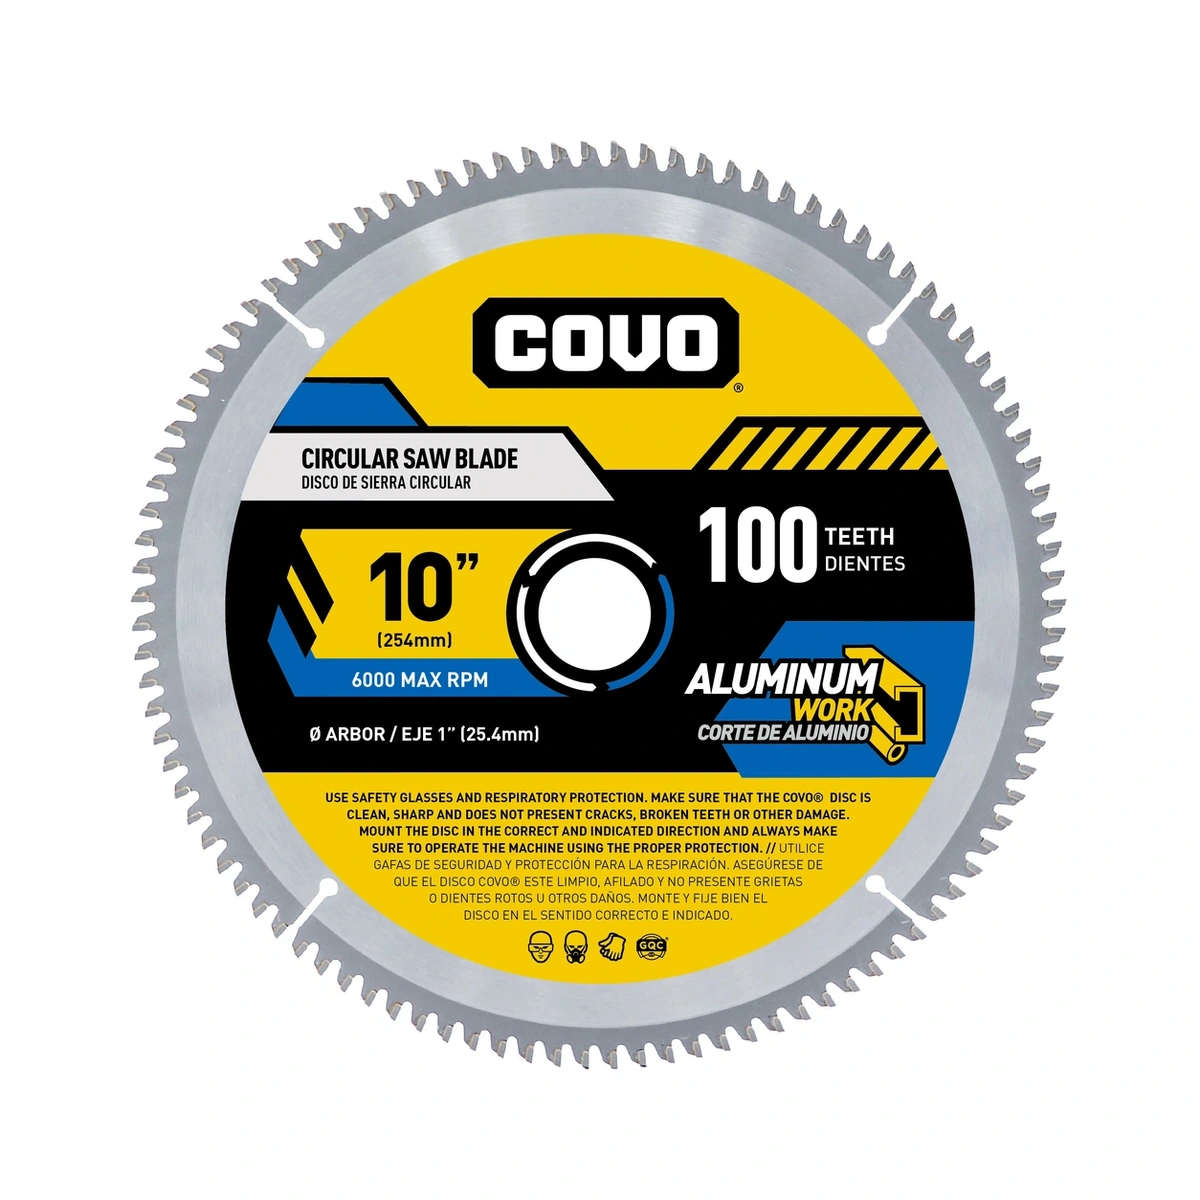
254mm / 10″ |
Number of Teeth | 100T |
Arbor Size | 25.4mm / 1″ |
Kerf Width | 2.8mm / 7/64″ |
Tooth Material | TCT |
Tooth Geometry | GCG |
Max. Safe Speed | 6000 rpm |
Reduction Ring | 20mm / 3/4″ |
Cutting Result | Fine Cut |
Compatible Machines

Application

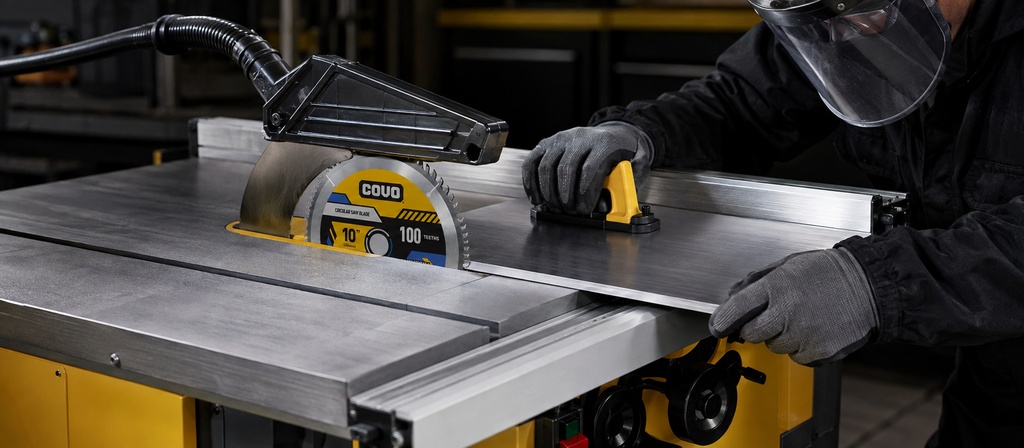

Safety Instructions
Eye protection
Please wear safety glasses
Hand Protection
Please wear protective gloves
Proper Disposal
Dispose of damaged or worn blades safely
Respiratory Protection
Please wear face respiratory mask
Frequently Asked Questions
The 100-tooth blade has smaller, denser teeth, and aluminum tends to gum up blades – making proper maintenance and operation especially critical.
Longevity & cutting tips:
- Always use lubrication: Lubrication is strongly recommended when cutting aluminum. Use a dedicated saw blade wax stick or a misting lubrication system. Lubrication reduces aluminum build-up on teeth, lowers friction heat, extends blade life, and delivers a smoother finish.
- Choose the right feed speed: Thicker aluminum requires a slower feed rate. Do not force the workpiece – let the blade cut at its own pace. Excessive pressure can overload and chip the carbide tips.
- Clean regularly: Aluminum cutting produces chips that can stick to the tooth gullets ("loading"), affecting cutting accuracy and chip evacuation. Clean debris from between teeth regularly.
- Use the right blade for the right material: This blade is for non-ferrous metals and non-metallic materials only – never use it on steel, stainless steel, or ferrous metals. Cutting ferrous metals will directly damage the carbide tips.
- Inspect teeth regularly: If cutting speed drops or finish becomes rough, check for chipped or worn teeth and have the blade professionally sharpened when needed.
Safety precautions (critical):
- Confirm max RPM: Machine speed must not exceed 6,000 RPM. Over-speeding is extremely hazardous!
- Keep guards in place: Metal cutting produces high-velocity chips – always keep machine guards installed.
- Wear full PPE: Safety goggles (for metal chips), ear protection (metal cutting is loud), dust mask, and gloves.
- Inspect the blade: Check for cracks, warping, or missing teeth before each use. Never use a damaged blade.
- Tighten securely: Ensure flange bolts are tightened and the blade is concentric with the arbor
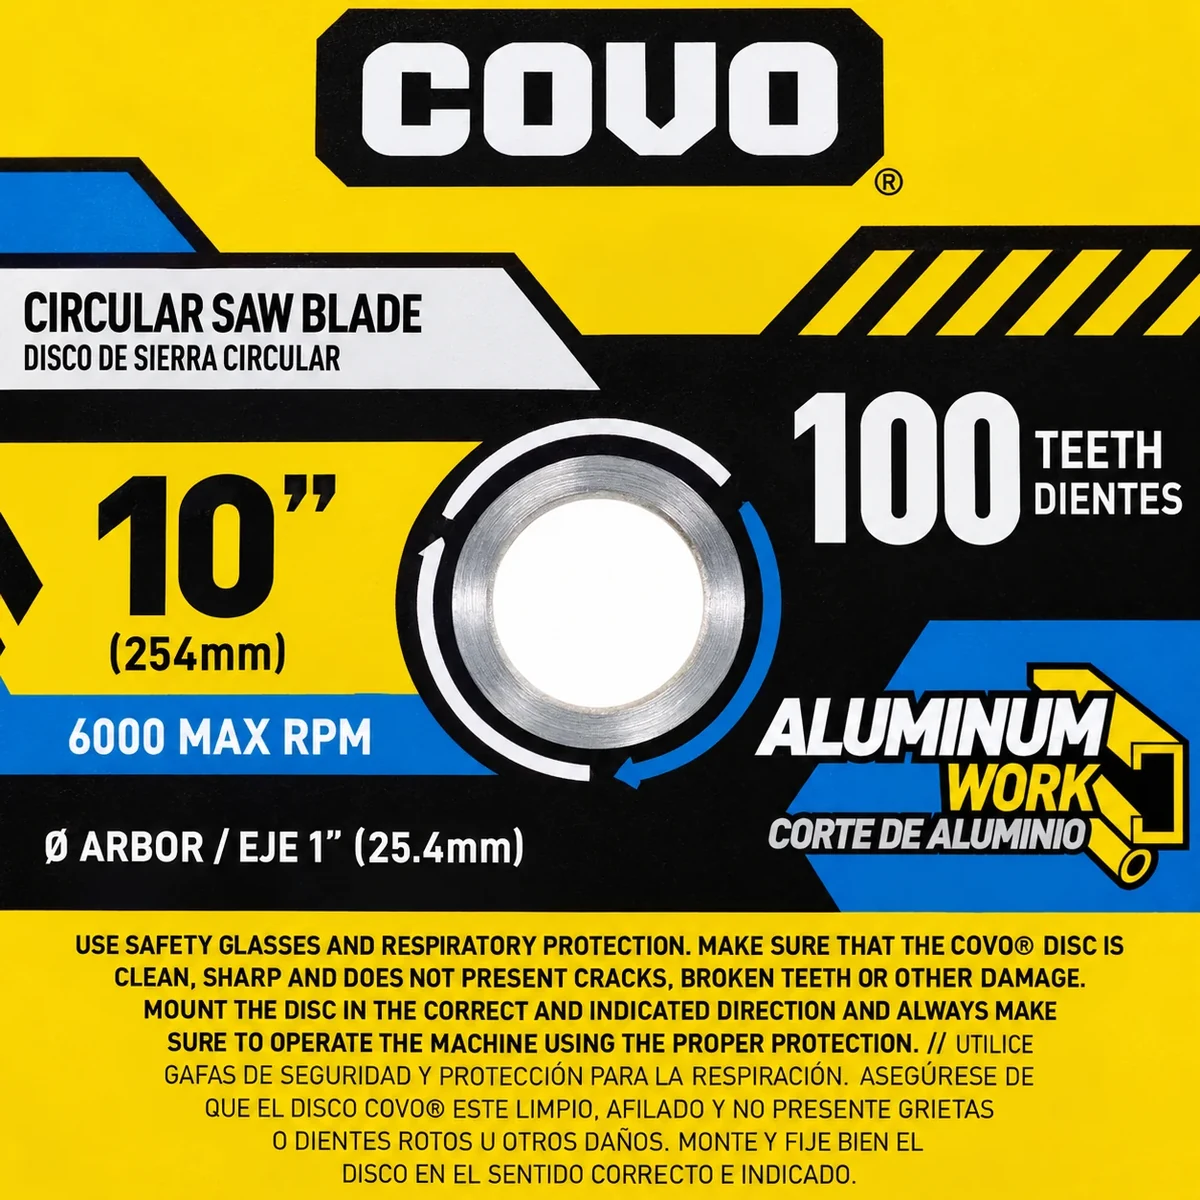
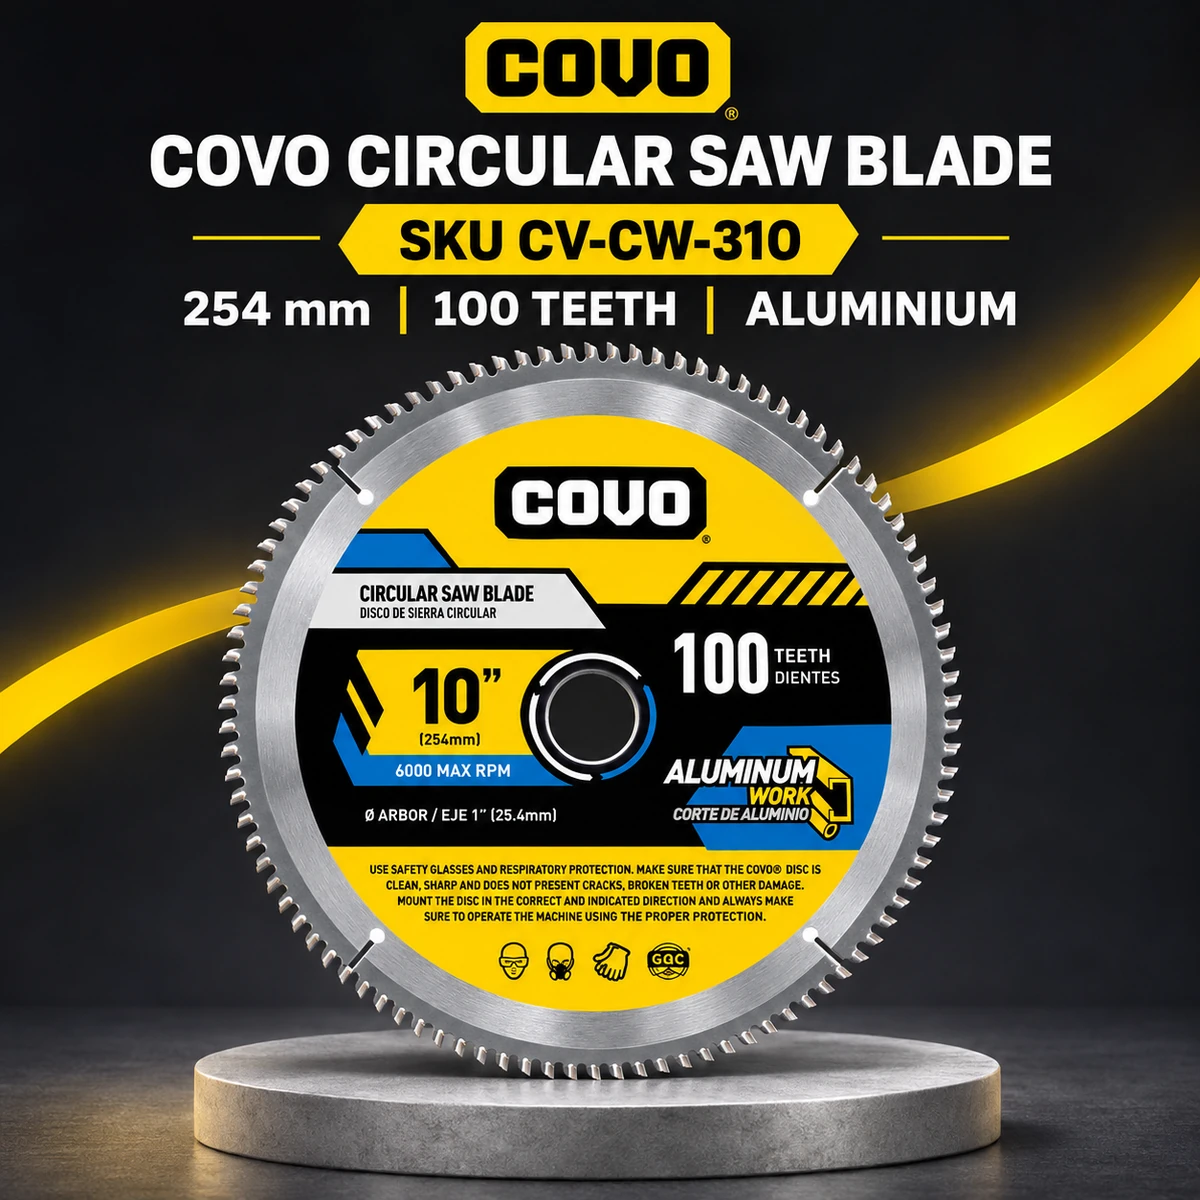
Here are the key specifications of this product:
| Specification | Detail |
|---|---|
| Blade Diameter | 10" (254mm) |
| Teeth Count | 100 Teeth |
| Arbor Size | 1" (25.4mm) |
| Max RPM | 6,000 RPM |
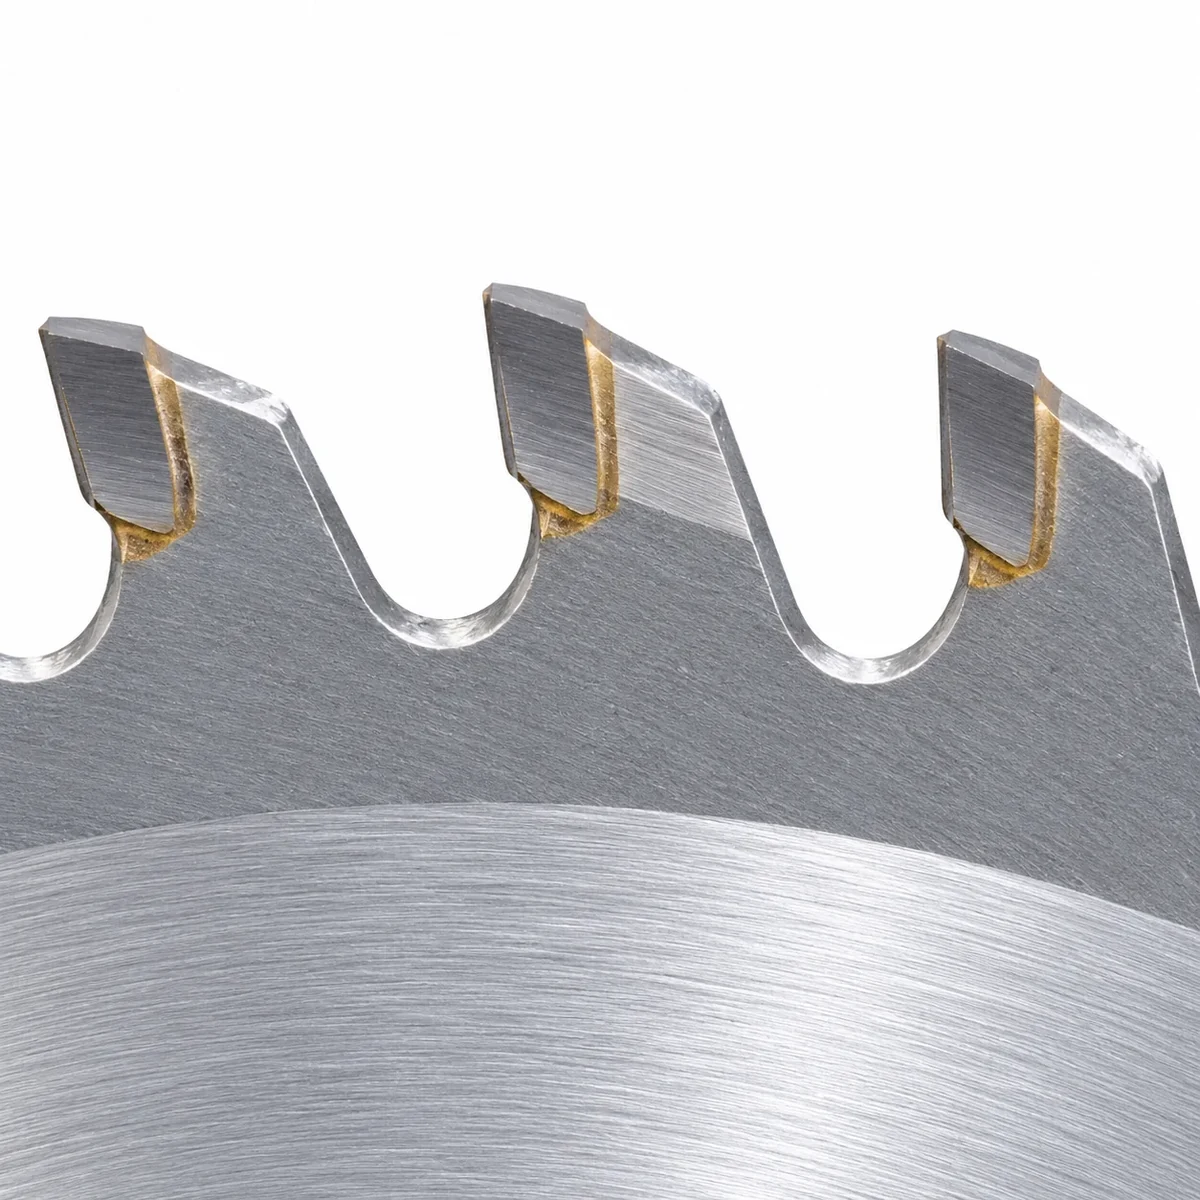
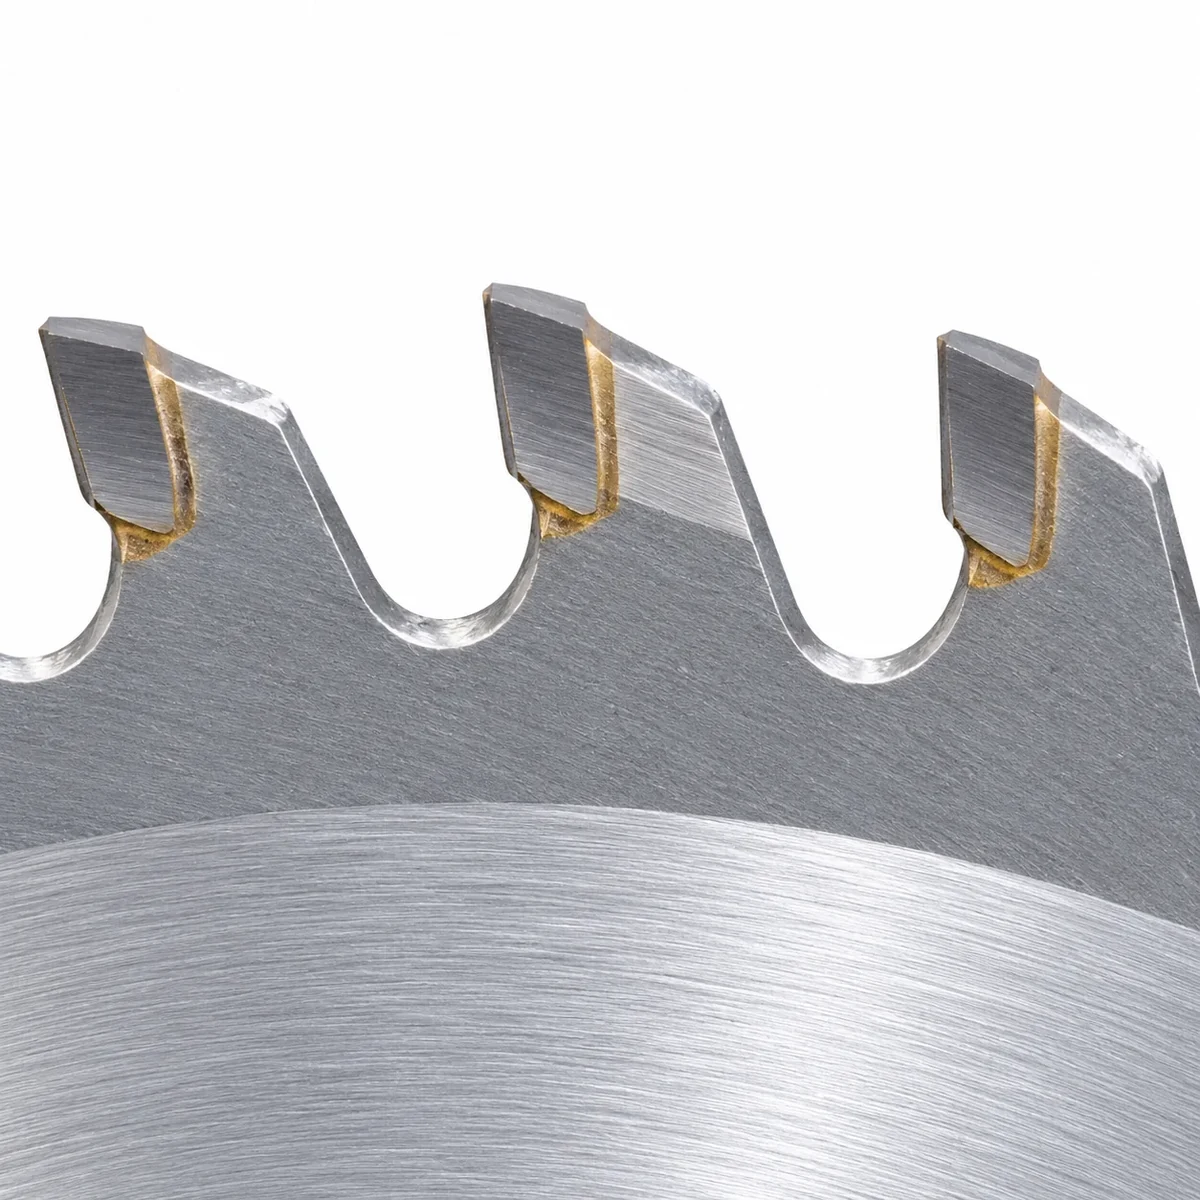
| Tooth Grind | TCG (Triple Chip Grind) |
| Kerf Width | Approx. 0.091–0.110" (2.3–2.8mm) |
Compatible Equipment:
- Table Saws
- Mitre Saws
- Chop Saws
Before installation, confirm these three points:
- Arbor match: Your machine's arbor must be 1" (25.4mm). If your machine has a different arbor size (e.g., 5/8" or 30mm), you may need a reduction ring (arbor adapter) .
- Max RPM: Your machine's no-load speed must not exceed 6,000 RPM. Over-speeding is not only dangerous but will also significantly reduce blade life.
- Equipment type: This blade is designed for woodworking-type saws (table saws, mitre saws, etc.) – not for low-speed cold saws.
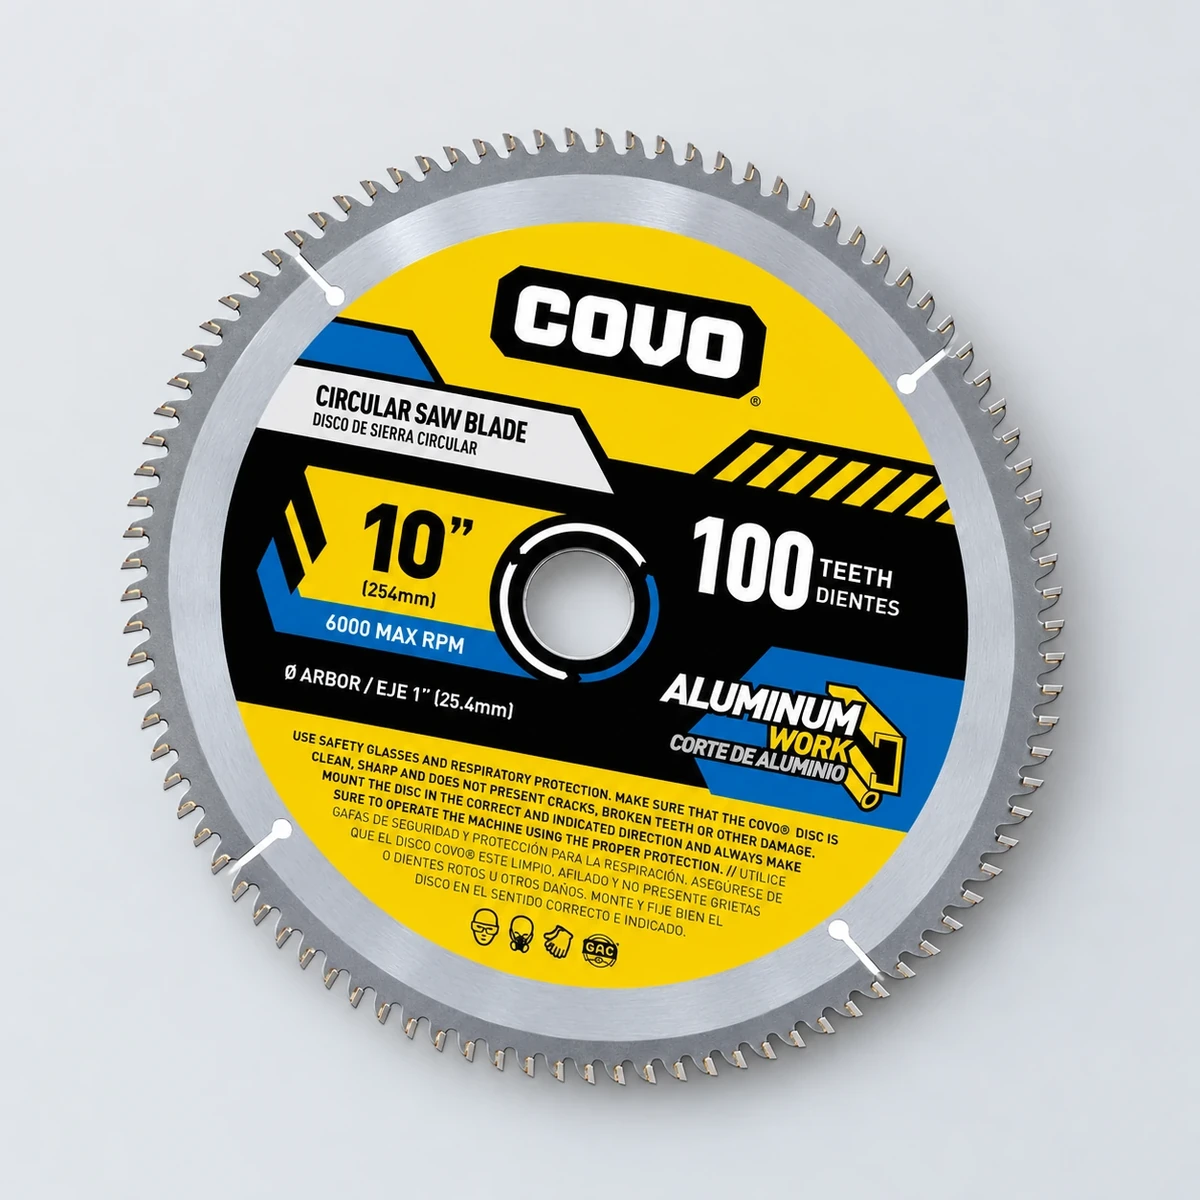
This 10" (254mm) 100-tooth carbide-tipped circular saw blade is engineered for high-precision, burr-free cutting of non-ferrous metals. It performs best on aluminum extrusions, aluminum sheets, aluminum bars, die-cast aluminum, copper, brass, bronze, and other non-ferrous metals. It is also suitable for plastics, Plexiglass, PVC, acrylics, and fiberglass.
Core advantages of 100 teeth:
| Teeth Count | Cutting Characteristics | Best Use |
|---|---|---|
| 40–60 Teeth | Faster cutting, rougher finish | Rough cutting, material removal |
| 80–100 Teeth (This Blade) | Ultra-smooth, burr-free, minimal chipping | Precision cutting, profile processing |
| 120+ Teeth | Mirror finish, slowest speed | Ultra-thin wall materials,极致 surface finish |
Tooth Design (TCG - Triple Chip Grind): This blade features a Triple Chip Grind (TCG) tooth geometry, with alternating trapezoidal and flat teeth. This design is specifically optimised for non-ferrous metals, effectively reducing burr formation during cutting and delivering clean, smooth cuts that require virtually no secondary finishing.
Advantage of the 10" (254mm) size: Compatible with table saws, mitre saws, and chop saws, with a single-pass cutting depth of approximately 80mm – ideal for batch processing of aluminum profiles and sheets.